 English
 中文简体
 Español
 Português
 Deutsch
 русский
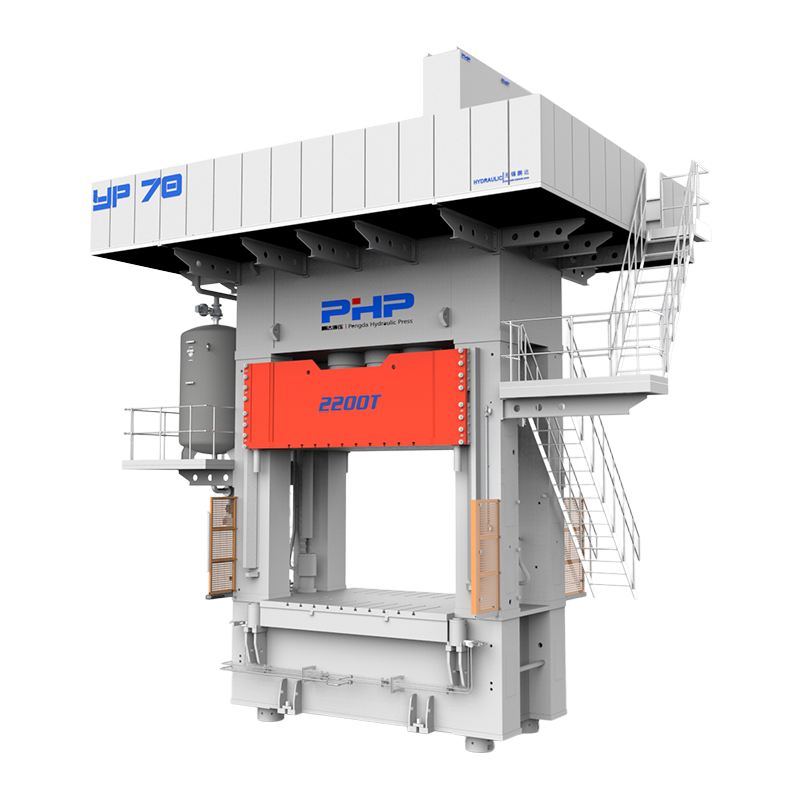

SMC Press Selection Guide
Press tonnage is usually the first specification buyers consider when selecting an SMC compression molding press. However, sufficient tonnage does not guarantee that a mold can actually be installed, opened, unloaded or integrated with automation.
Platen size, stroke and daylight define the physical working envelope of the press. If any one of these parameters is undersized, a press with otherwise sufficient force may still be unsuitable for the application.
Content
- 1 1. Why Tonnage Alone Is Not Enough
- 2 2. How to Select the Correct Platen Size
- 3 3. How Much Stroke Does an SMC Press Need?
- 4 4. What Is Daylight and How Should It Be Selected?
- 5 5. Stroke vs Daylight: What Is the Difference?
- 6 6. Mold Weight Is Also Part of Press Sizing
- 7 7. Automation Changes Stroke and Daylight Requirements
- 8 8. Bigger Platen, Stroke and Daylight Are Not Automatically Better
- 9 9. Practical Example: Sizing an SMC Press Around the Mold
- 10 10. What Information Should Buyers Provide to the Press Manufacturer?
- 11 11. Common SMC Press Sizing Mistakes to Avoid
- 12 Size the SMC Press Around the Mold, Not Just the Tonnage
- 13 SMC Press Configuration from Wuxi PengdaHZ
- 14 Frequently Asked Questions
- 14.1 How much larger should the press platen be than the SMC mold?
- 14.2 What is daylight in a hydraulic press?
- 14.3 What is the difference between stroke and daylight?
- 14.4 How do I calculate the required stroke for an SMC mold?
- 14.5 How do I determine the required daylight?
- 14.6 Can an SMC mold be larger than the press platen?
- 14.7 Does a larger platen require a stiffer press frame?
- 14.8 How does mold weight affect SMC press selection?
- 14.9 How much opening is needed for robotic part removal?
- 14.10 Should I leave extra stroke and daylight for future molds?
1. Why Tonnage Alone Is Not Enough
A buyer may know that the application requires a 500-ton, 1000-ton or 2000-ton press, but this answers only the force requirement.
The machine must also physically accommodate the mold and provide enough movement for loading, ejection and part removal.
01
Press Tonnage
Determines the maximum available compression force and should be matched to projected molding area and required molding pressure.
02
Platen Size
Determines whether the mold footprint can be properly supported, mounted and connected.
03
Stroke
Determines how far the moving platen can travel during opening and closing.
04
Daylight
Determines the maximum open space available between the platens for the mold and handling clearance.
Part Size→Mold Size→Platen Size
Mold Height+Opening Requirement→Stroke & Daylight
2. How to Select the Correct Platen Size
Platen size should never be selected by looking only at finished part dimensions. The actual mold is normally larger than the component because it includes mold steel, heating circuits, mounting areas, ejector structures and other features.
Start with the Mold Footprint
The first information required is the overall mold length and width.
For example, a molded SMC panel measuring 1100 × 700 mm may require a mold measuring 1450 × 1050 mm or more depending on its tooling design.
The platen must provide enough usable area to properly support this tooling.
| Mold Requirement | Platen Consideration |
| Overall Mold Footprint | The working surface must support the complete mold |
| Clamping | Allow space for clamps, T-slots or mounting bolts |
| Heating Connections | Provide clearance for electrical or thermal connections |
| Ejector Connections | Confirm ejector layout and access |
| Maintenance Access | Do not position the mold so tightly that servicing becomes difficult |
A platen only slightly larger than the mold may create installation problems.
Enough surrounding space should be available for clamping, wiring, heating lines and maintenance rather than sizing the platen exactly to the mold footprint.
Consider Mold Position and Off-Center Loading
Ideally, the mold and major cavity load should be positioned close to the center of the press.
If the tooling must operate significantly off-center, the press structure may experience greater eccentric loading, which can affect platen deflection and loaded parallelism.
For large or asymmetric SMC molds, platen dimensions should therefore be evaluated together with frame stiffness and allowable off-center loading.
3. How Much Stroke Does an SMC Press Need?
Press stroke is the travel distance of the moving platen. It is not the same as part height and it should not be selected from mold height alone.
The required stroke depends on how much movement is needed to:
- open the mold;
- release the molded component;
- operate the ejector;
- remove the part manually or robotically;
- load the next SMC charge;
- load inserts if required.
Required Stroke ≈ Part Removal Requirement + Ejection Requirement + Handling Clearance
This is a practical sizing concept rather than a universal formula. Final stroke should be confirmed from the mold drawing and actual loading/unloading method.
If Stroke Is Too Short
- the part may be difficult to remove;
- robot grippers may not enter safely;
- ejector movement may interfere with handling;
- mold maintenance becomes more difficult.
If Stroke Is Excessively Long
- machine structure becomes larger;
- opening and closing travel can increase;
- cycle time may increase unnecessarily;
- equipment cost may rise without production benefit.
More stroke is not automatically better. The optimum stroke is enough to open, eject and handle the part reliably without adding unnecessary machine travel.
4. What Is Daylight and How Should It Be Selected?
Daylight generally refers to the maximum open distance between the upper and lower platen working surfaces when the press is fully open.
It defines the total vertical space available for the closed mold plus the opening clearance required by the production process.
Required Daylight ≥ Closed Mold Height + Required Opening Clearance
Suppose an SMC mold has a closed height of 650 mm and the process requires approximately 500 mm of opening clearance for unloading and loading.
Closed Mold Height 650 mm+Required Opening Clearance 500 mm=Initial Daylight Requirement 1150 mm
Additional clearance may still be required depending on robot tooling, ejector position, insert loading and future automation.
This is a geometry example, not a universal machine specification.
Final daylight should always be confirmed against the actual mold drawing and handling envelope.
5. Stroke vs Daylight: What Is the Difference?
Stroke and daylight are often confused during press inquiries, but they describe different machine dimensions.
| Parameter | What It Means | Main Function |
| Stroke | Travel distance of the moving platen | Determines available opening movement |
| Daylight | Maximum open distance between platen working surfaces | Accommodates mold height plus open clearance |
| Closed Mold Height | Overall mold thickness when completely closed | Determines required closed press geometry |
| Platen Size | Length and width of the press working surface | Determines mold footprint capacity |
Consider a simplified press with 1200 mm of daylight and 500 mm of stroke. Depending on the press architecture, its closed-position working space would relate closely to the difference between these two dimensions.
However, machine manufacturers may define certain dimensional specifications differently, so buyers should always confirm the press drawing instead of comparing brochure numbers alone.
6. Mold Weight Is Also Part of Press Sizing
Mold dimensions determine whether the tool fits, but mold weight determines whether the press and handling system can safely support and move it.
Important values include:
- total mold weight;
- upper mold half weight;
- lower mold half weight;
- moving platen allowable load;
- mold-changing method.
Why Upper Mold Weight Matters
The upper mold half is normally attached to the moving platen. A heavy upper mold adds moving mass and places additional demands on the guiding, hydraulic and structural systems.
Large molds may also require special installation arrangements such as:
Overhead Crane
Mold Change Cart
Roller Table
Quick Clamping
These requirements can influence the frame opening, platen height, side access and overall production-line layout.
7. Automation Changes Stroke and Daylight Requirements
A press that is perfectly adequate for manual production may become too small vertically once robotic loading and unloading are introduced.
Automation may require additional clearance for:
- robot end-of-arm tooling;
- part grippers;
- vacuum cups;
- SMC charge loading trays;
- insert handling;
- release-agent spraying;
- vision systems.
Plan Phase 2 Automation During Phase 1 Press Sizing
If robotic loading or unloading is likely to be added later, its clearance envelope should be considered when the press is originally specified.
Robot Approach→Gripper Clearance→Part Removal→Next Charge Loading
Retrofitting automation later is much easier when sufficient daylight, stroke and side access were reserved from the beginning.
8. Bigger Platen, Stroke and Daylight Are Not Automatically Better
Oversizing the press working envelope can appear attractive because it creates more theoretical flexibility, but every increase affects machine design.
| Oversized Parameter | Possible Consequence |
| Excessively Large Platen | Greater structural span, higher stiffness requirement and higher machine cost |
| Excessive Stroke | Longer unnecessary movement and potentially longer cycle time |
| Excessive Daylight | Larger frame and machine height |
| Excessive Mold Capacity Margin | Higher capital cost without guaranteed production benefit |
The right press is not the machine with the largest numbers. It is the machine whose working envelope matches the mold, handling system and production process.
9. Practical Example: Sizing an SMC Press Around the Mold
Consider a manufacturer planning an SMC component with the following preliminary production data:
Finished Part 1200 × 800 mm
Mold Footprint 1500 × 1100 mm
Closed Mold Height 700 mm
Required Part Removal 450 mm
Robot Gripper Height 180 mm
Production Mode Automatic
Step 1: Platen Size
The platen must be larger than the 1500 × 1100 mm mold footprint and provide usable surrounding space for mounting, connections and servicing.
Step 2: Stroke
The required opening must consider not only the molded part but also the ejector and robot gripper. The machine should provide enough travel for reliable removal without excessive unnecessary motion.
Step 3: Daylight
The 700 mm closed mold height must be combined with the required opening clearance. Depending on the robot path and ejector arrangement, a preliminary daylight requirement might fall in the 1200–1400 mm range before the final engineering drawing is confirmed.
The example above is intended to demonstrate the sizing method. Final press dimensions should be confirmed using the real mold drawing, upper and lower mold weights, ejector design and complete robot collision envelope.
10. What Information Should Buyers Provide to the Press Manufacturer?
Sending only the message “Need 1000T SMC press” is rarely enough for accurate equipment configuration.
A more useful technical inquiry includes:
| Data to Provide | Why It Matters |
| Part L × W × H | Defines the basic component envelope |
| Projected Molding Area | Used to calculate required press force |
| Mold L × W | Determines platen size |
| Closed Mold Height | Required for daylight sizing |
| Total Mold Weight | Affects structural and handling requirements |
| Upper Mold Weight | Affects moving platen loading |
| Required Opening | Influences stroke and daylight |
| Ejector Stroke | Defines part-release requirements |
| Robot / Gripper Dimensions | Defines automation clearance |
| Heating Connections | Affects mold access and platen layout |
| Target Cycle Time | Influences motion and hydraulic configuration |
| Future Mold Range | Helps determine reasonable capacity margin |
11. Common SMC Press Sizing Mistakes to Avoid
01
Selecting the Press by Tonnage Only
Adequate force does not guarantee adequate mold space.
02
Making the Platen Only Slightly Larger Than the Mold
This can leave insufficient space for clamps, heating lines and maintenance.
03
Ignoring Robot Clearance
A mold may open far enough for manual unloading but not for a gripper to enter safely.
04
Confusing Stroke with Daylight
The two dimensions describe different parts of the press working envelope.
05
Ignoring Upper Mold Weight
Heavy upper tooling affects moving mass, guidance and structural requirements.
06
Buying Excessive Stroke and Daylight
Oversizing can increase equipment cost and unnecessary machine movement.
07
Ignoring Future Molds
A reasonable margin can prevent an otherwise good press from becoming unusable for the next project.
Size the SMC Press Around the Mold, Not Just the Tonnage
A properly selected SMC press should satisfy both the force requirement and the physical production envelope.
Tonnage+Platen Size+Stroke+Daylight+Mold Weight+Automation Clearance
The best approach is to work from the part drawing and mold drawing outward. This allows the press structure, table dimensions, stroke, daylight and handling system to be configured around the real production requirement rather than a nominal tonnage alone.
SMC Press Configuration from Wuxi PengdaHZ
Wuxi PengdaHZ Intelligent Equipment Co., Ltd. develops hydraulic press systems for SMC, BMC and composite compression molding applications.
When selecting a new SMC press, our equipment evaluation can consider required tonnage together with mold dimensions, mold weight, closed mold height, platen size, stroke, daylight, loading method and automation requirements.
For a more accurate machine configuration, prepare your part drawing, mold drawing, SMC material, required molding pressure, target cycle time and planned loading/unloading method.
Visit wuxipd.com for more information about customized SMC compression molding presses and composite molding equipment.
Frequently Asked Questions
How much larger should the press platen be than the SMC mold?
There is no universal margin. The platen should fully support the mold while providing sufficient space for clamping, mounting, heating connections, ejector connections and maintenance access.
What is daylight in a hydraulic press?
Daylight generally refers to the maximum open distance between the working surfaces of the upper and lower platens. It must accommodate the mold height plus the opening space required for production.
What is the difference between stroke and daylight?
Stroke is the travel distance of the moving platen. Daylight is the maximum open distance available between the platen working surfaces.
How do I calculate the required stroke for an SMC mold?
Consider the mold opening required for part release, ejector movement, manual or robotic handling, charge loading and any insert-loading requirements.
How do I determine the required daylight?
Start with the closed mold height and add the opening clearance needed for ejection, part removal, robot tooling and loading. Final dimensions should be confirmed against the mold and automation drawings.
Can an SMC mold be larger than the press platen?
This is generally undesirable because the tool requires proper structural support and mounting. The final arrangement should always be reviewed by the press and tooling engineers.
Does a larger platen require a stiffer press frame?
As working span increases, structural stiffness and platen deflection become increasingly important, especially with large or off-center molds.
How does mold weight affect SMC press selection?
Total mold weight affects support and handling requirements, while upper mold weight influences the moving platen, guidance system and dynamic load.
How much opening is needed for robotic part removal?
Opening should account for the molded part, ejector position, gripper dimensions, robot approach path and collision clearance. The complete automation envelope should be checked rather than the part height alone.
Should I leave extra stroke and daylight for future molds?
A reasonable margin can be useful when future mold requirements are known or likely, but excessive oversizing increases machine size and cost. Future tooling should be estimated before deciding how much additional capacity is justified.